Low-Risk Activewear Capsule Runs
Launch proprietary fitness collections with low starting volumes or zero-MOQ sublimated capsules, minimizing inventory overhead.
Get in touch
Sales line+92 329 6140058 Emailbusiness@benjima.com OfficeRungpura, Sialkot, Punjab, Pakistan Working hoursMonday to Saturday, 9:00 to 18:00 PKTFollow
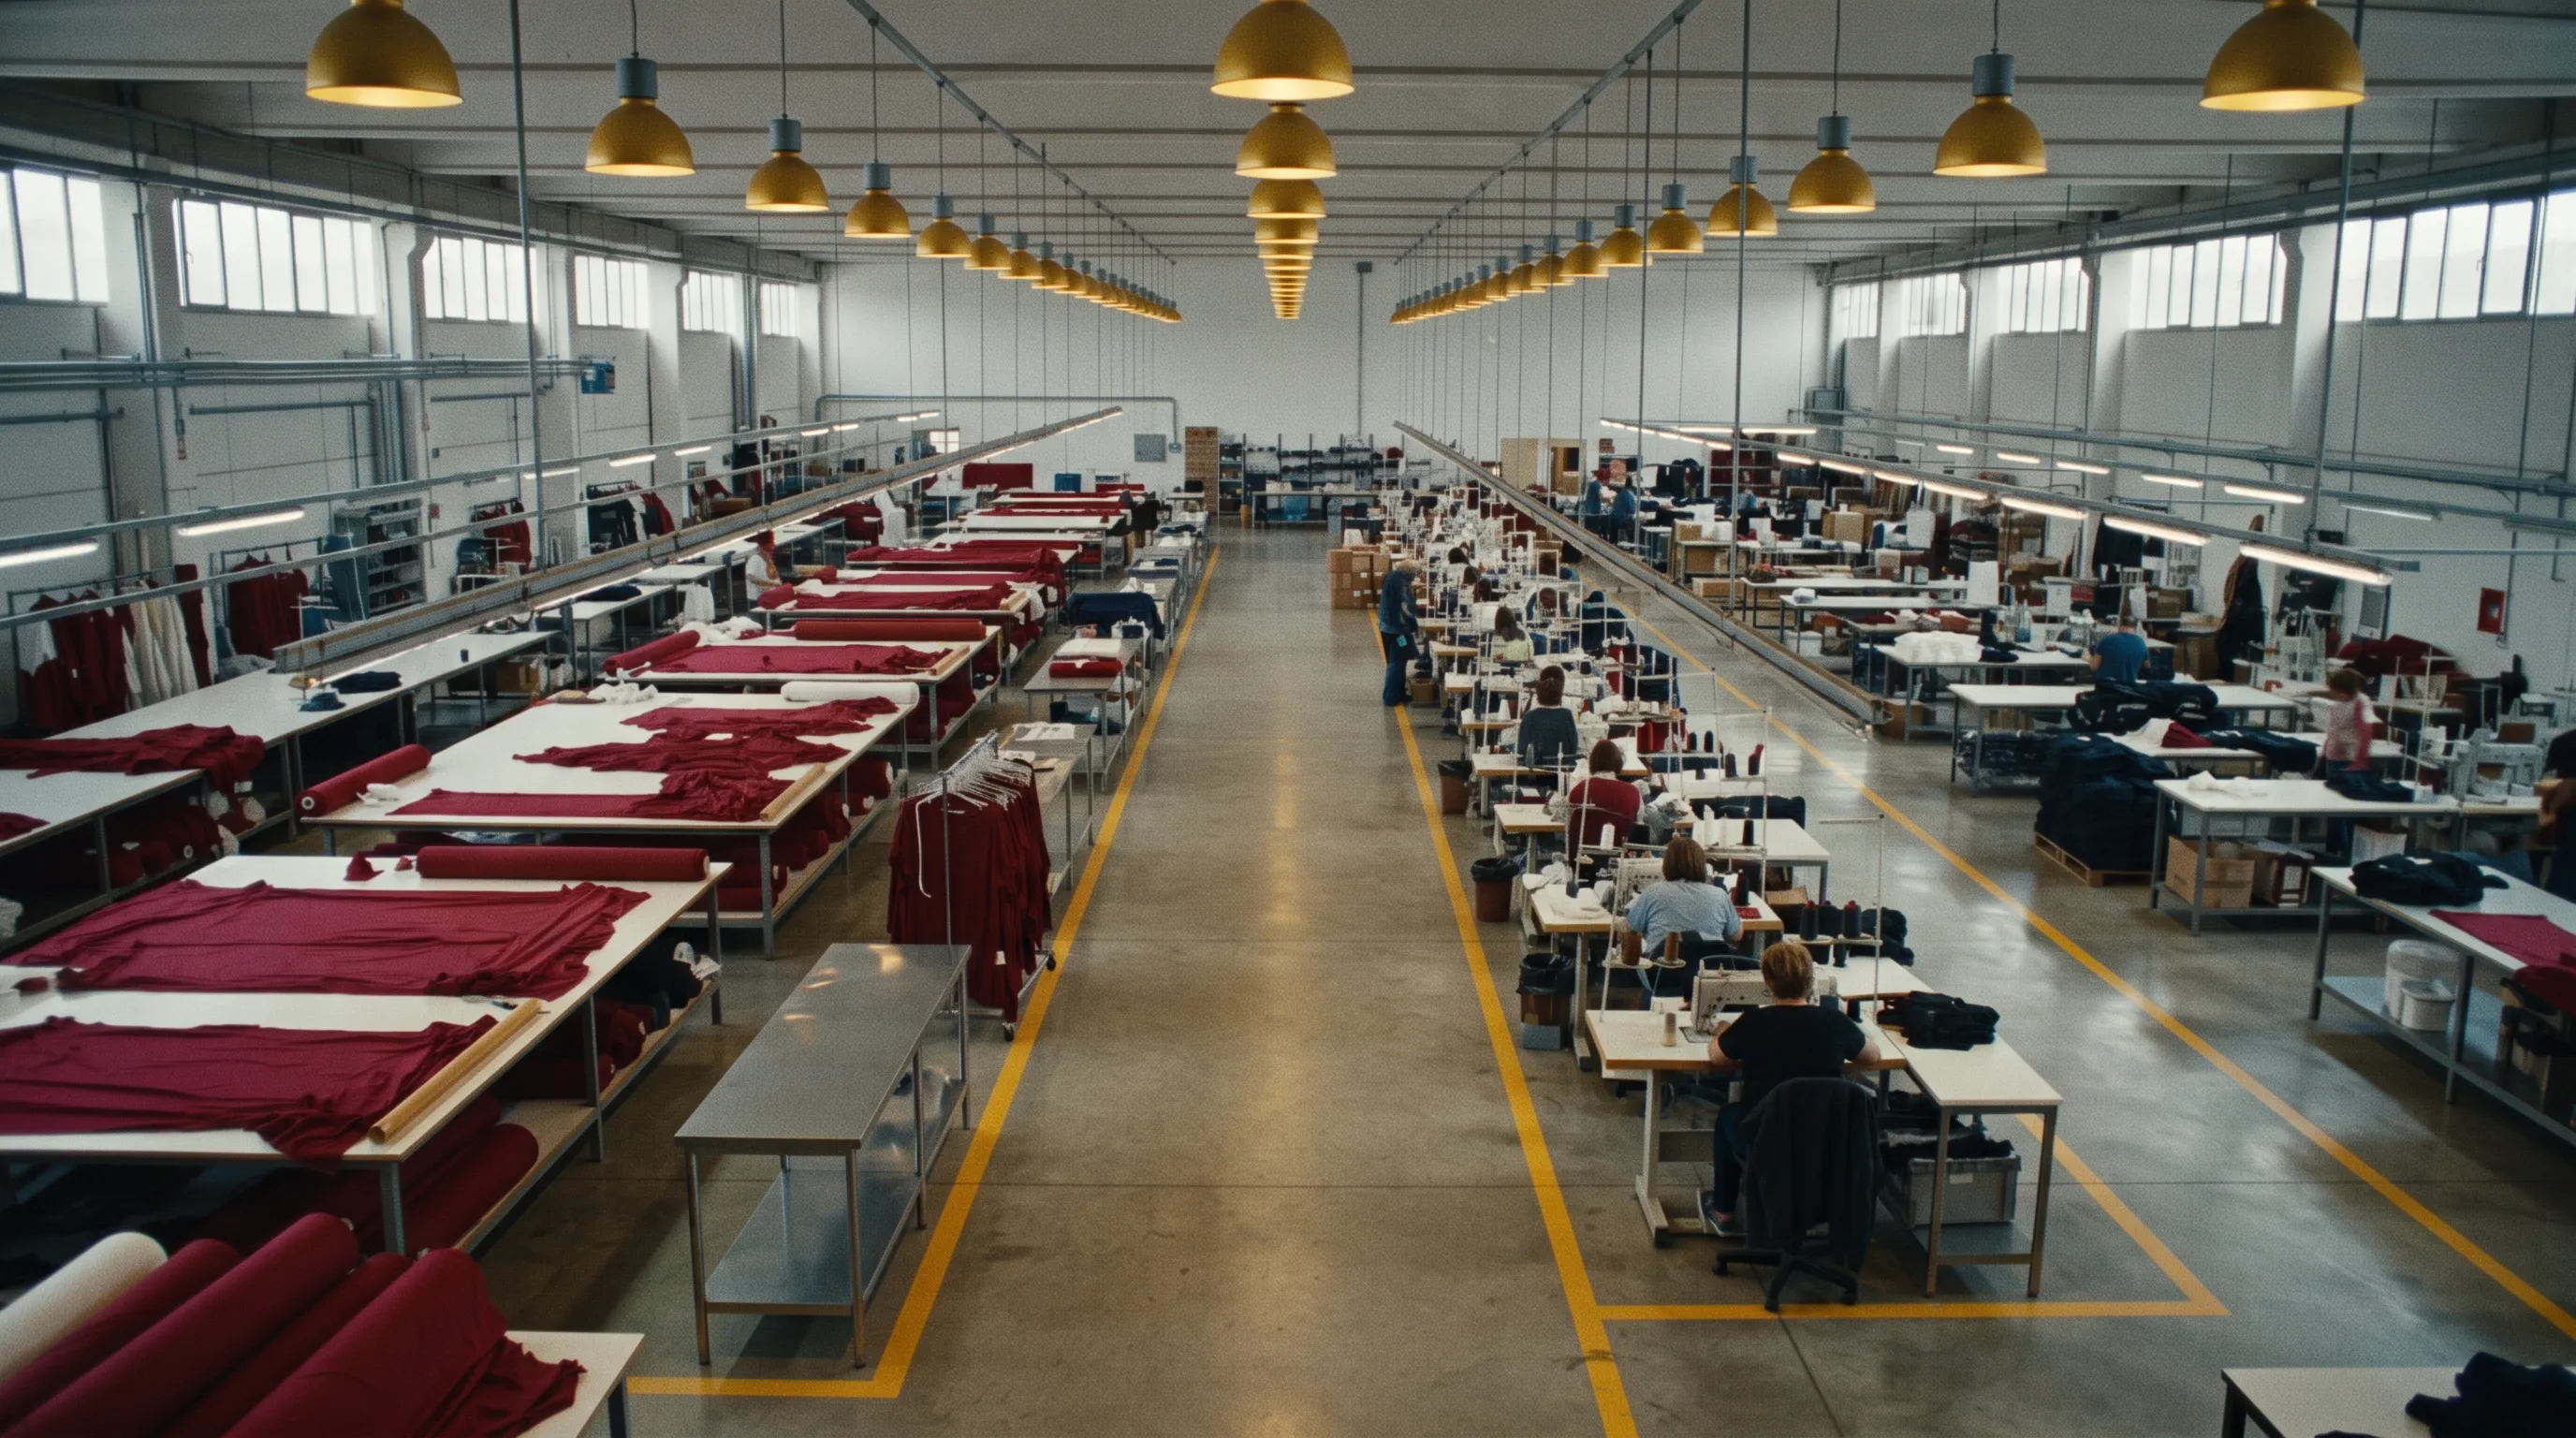
Benjima operates as a premier full-service custom sportswear private label manufacturer engineered specifically for emerging fitness apparel brands, activewear startups, gym chains, and established athletic labels worldwide. Our state-of-the-art production facility delivers end-to-end original equipment manufacturing (OEM) and original design manufacturing (ODM) services, combining premium performance knits, four-way stretch nylon-spandex, seamless compression textiles, and organic cotton blends. Apparel entrepreneurs gain the ability to launch cohesive, retail-grade athletic collections without the traditional capital burdens of massive inventory investments.
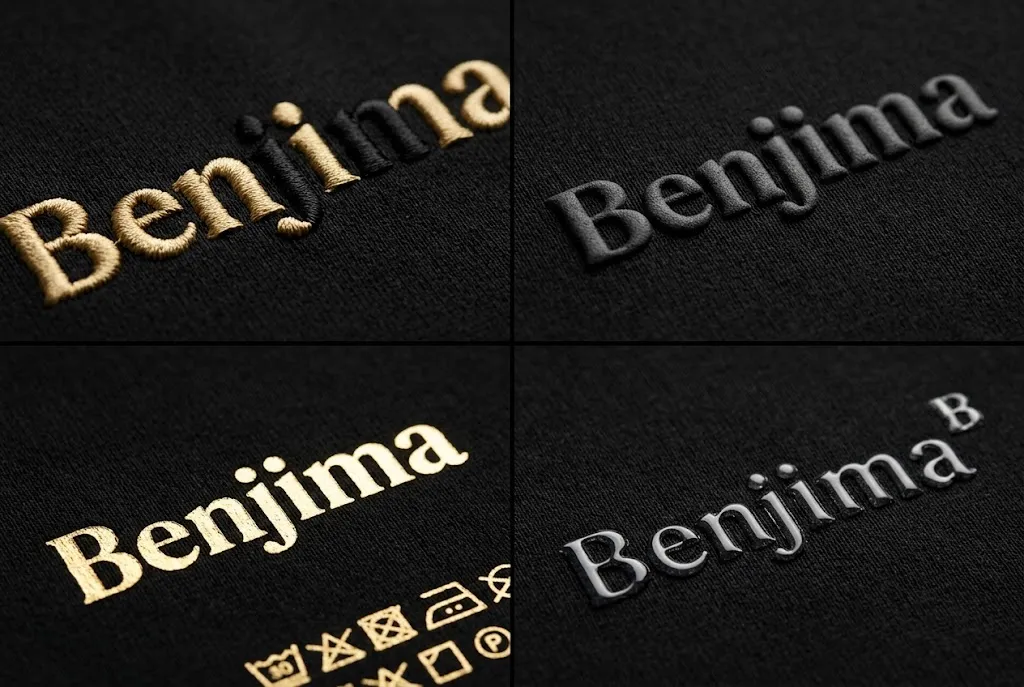
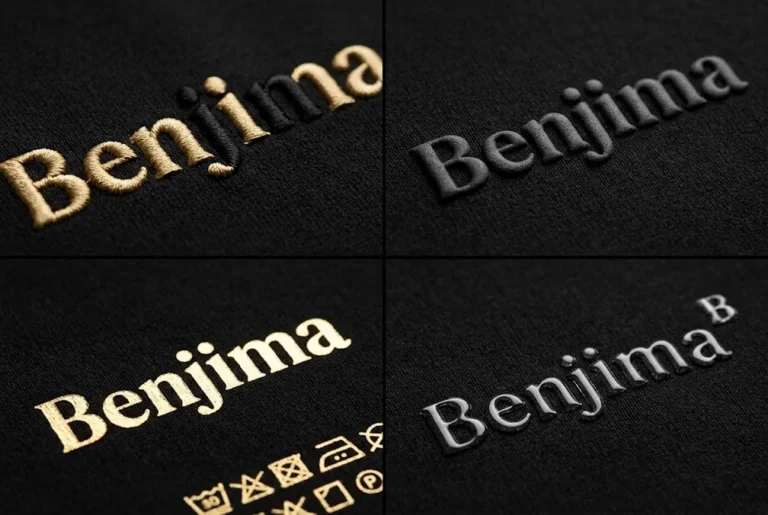
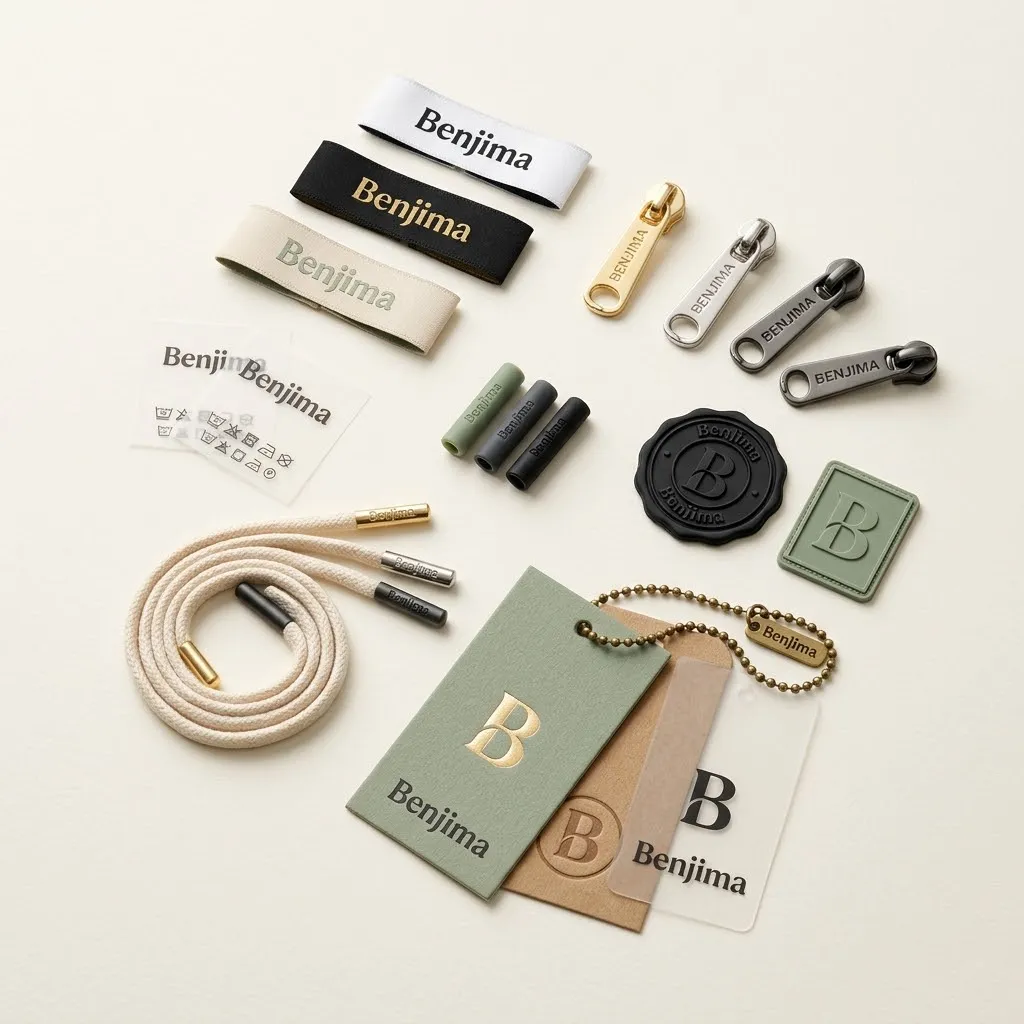
Every private label garment undergoes rigorous manufacturing protocols, including custom tech pack development, specialized fabric sourcing, precision pattern grading, and comprehensive bespoke branding. We equip your brand with custom woven neck labels, heat-transfer care tags, branded silicone aglets, custom engraved zipper pulls, and sustainable branded polybag packaging. Our diverse decorative capabilities encompass full dye sublimation, puff screen printing, high-density 3D embroidery, and metallic foil stamping, ensuring your collections reflect uncompromising retail excellence.
We eliminate industry entry barriers for independent activewear founders, athletic gym owners, and creative directors with flexible zero-to-low minimum order quantities and complimentary photorealistic 3D digital mockups. Whether testing a boutique capsule collection of fifty pieces or scaling commercial production into thousands of units, our direct factory provides dependable two to three week turnarounds and honest wholesale factory pricing.
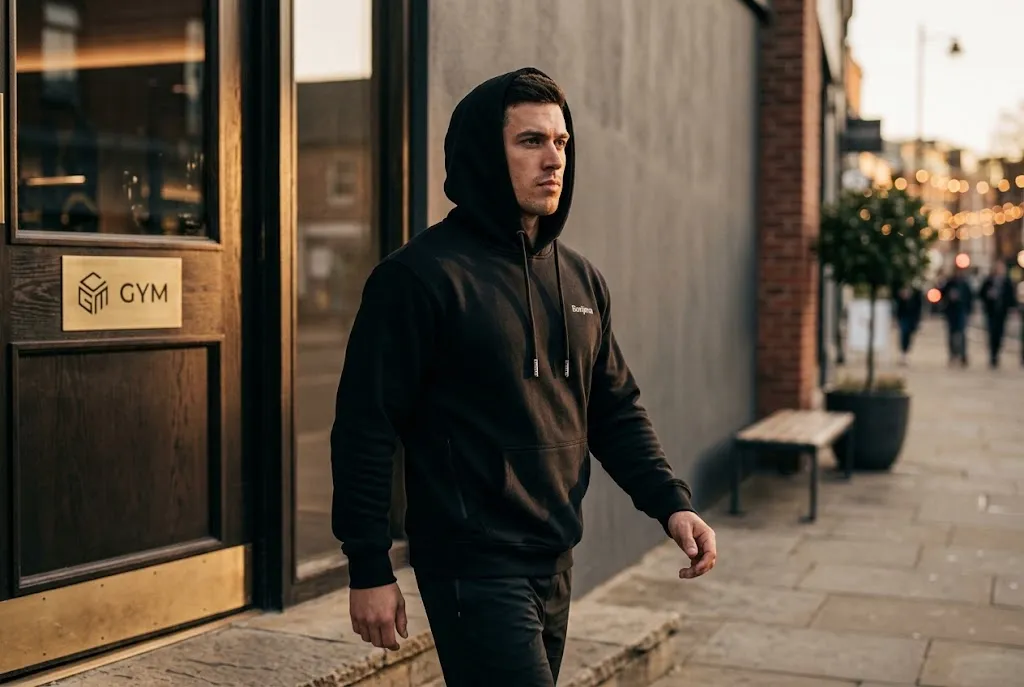
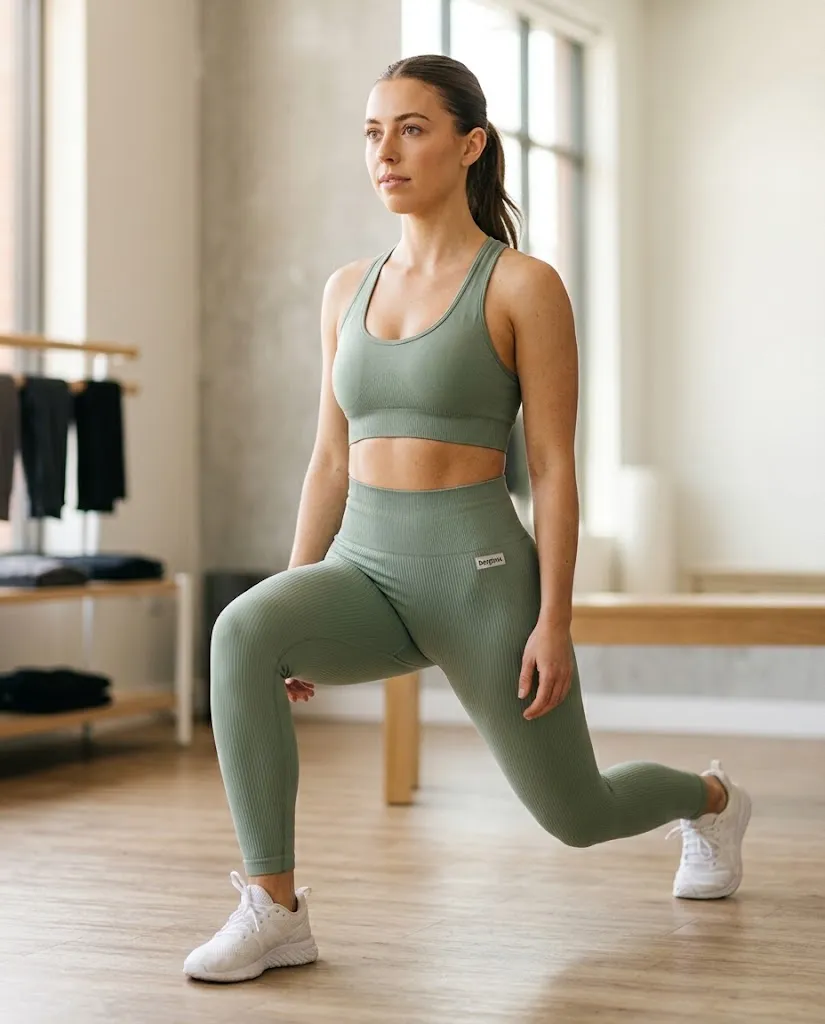
Launching and scaling a competitive athletic apparel brand requires a manufacturing partner that understands technical textiles, contemporary streetwear-athletic silhouettes, and meticulous brand presentation. Our comprehensive cut-and-sew services provide end-to-end support across the entire product lifecycle, from initial tech pack drafting and prototype sampling to bulk textile dyeing and precision assembly. Every garment pattern is engineered with ergonomic contours, flatlock anti-chafing construction, and premium stretch-recovery memory.
Collaborating directly with our private label production engineers gives brand founders total creative autonomy over fabric compositions, GSM weights, custom color matching via Pantone references, and bespoke packaging touches. We manufacture matching sports bras, high-waisted seamless leggings, oversized gym hoodies, performance pump tees, and athletic joggers under one cohesive collection vision. Your apparel brand enters the global fitness marketplace looking refined, authoritative, and ready to compete with household athleisure names.
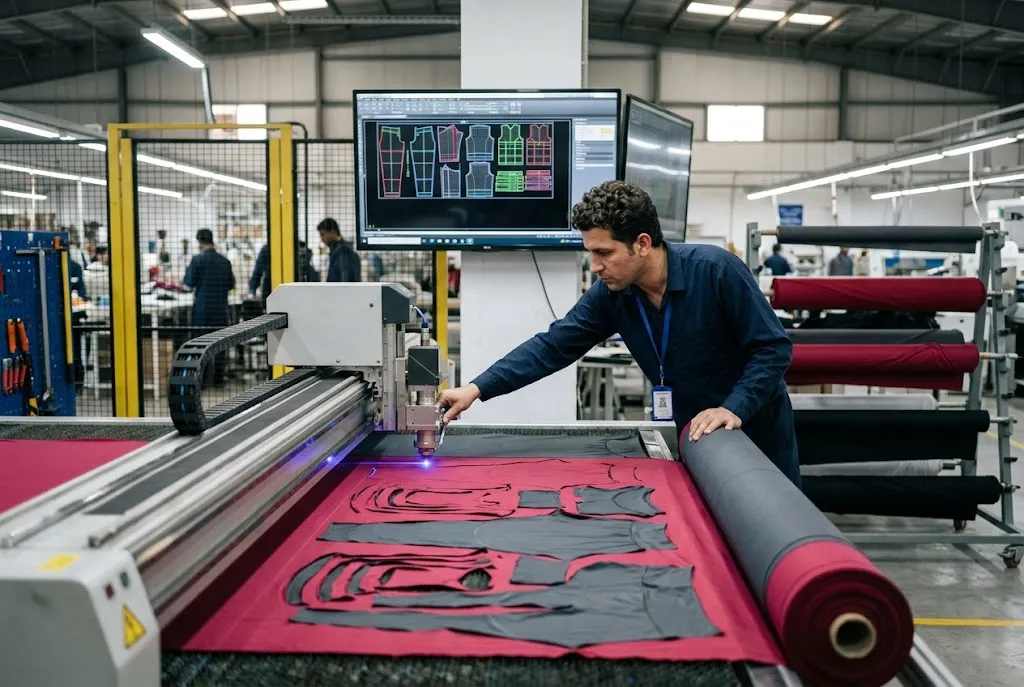
Our manufacturing video highlights how raw technical yarns and premium textiles transform into finished private label activewear collections inside our certified manufacturing facility. You will observe our pattern designers draft computerized tech packs and digital CAD markers before routing cut files to automated high-precision laser cutters. Specialized textile printing technicians operate large-format sublimation presses and multi-station screen printing carousels using certified non-toxic, eco-friendly inks.
The camera documents master seamstresses assembling complex athletic garments utilizing six-thread flatlock machines, seamless circular knitting looms, and bar-tack stations. Custom branding specialists apply woven satin neck labels, heat-sealed care instructions, and custom hang tags with surgical precision. Quality assurance inspectors examine each piece under calibrated illumination tables, evaluating seam tensile strength, color consistency, and dimensional tolerances before steam pressing, folding, and packing in custom retail bags.
Discover the transparent craftsmanship behind our private label OEM operations and see why leading global athletic brands trust Benjima as their dedicated manufacturing engine.
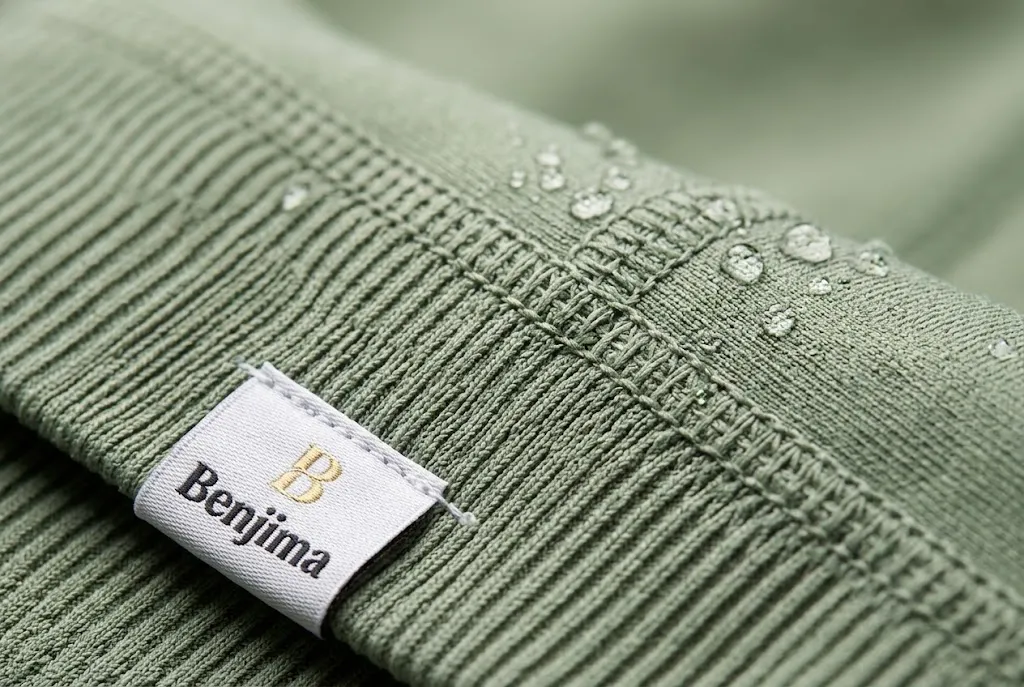
We combine technical textile innovation with flexible direct factory manufacturing to build thriving, profitable athletic apparel brands.
Launch proprietary fitness collections with low starting volumes or zero-MOQ sublimated capsules, minimizing inventory overhead.
Transform brand sketches into professional CAD tech packs, custom woven neck label templates, and packaging proofs.
Direct factory control ensures custom private label apparel ships in 2-3 weeks, protecting your commercial marketing launch dates.
Eliminate sourcing middlemen and trading agents to capture optimal retail profit margins straight from our manufacturing floor.
Our premium nylon-spandex, micro-poly, and combed French terry fabrics deliver high-compression elasticity and buttery-soft hand feels demanded by discerning fitness consumers. The technical weave provides squat-proof opacity, four-way stretch mobility, and rapid moisture wicking that excels in high-intensity training environments and casual lifestyle settings.
Eco-friendly dye sublimation, high-density silicone prints, and fine-gauge embroidery integrate seamlessly into the textiles. Custom logo badges, inner neck prints, and branded aglets never peel, crack, or fade under commercial washing, ensuring your label builds lifelong consumer trust and pristine market prestige.
Request a quoteBrowse authentic private label athletic collections, bespoke gym wear, seamless yoga apparel, and athleisure garments manufactured for independent brands worldwide.
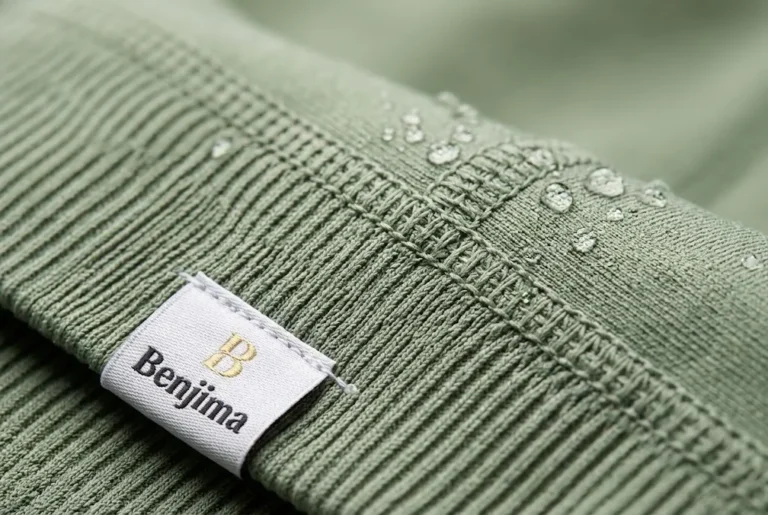
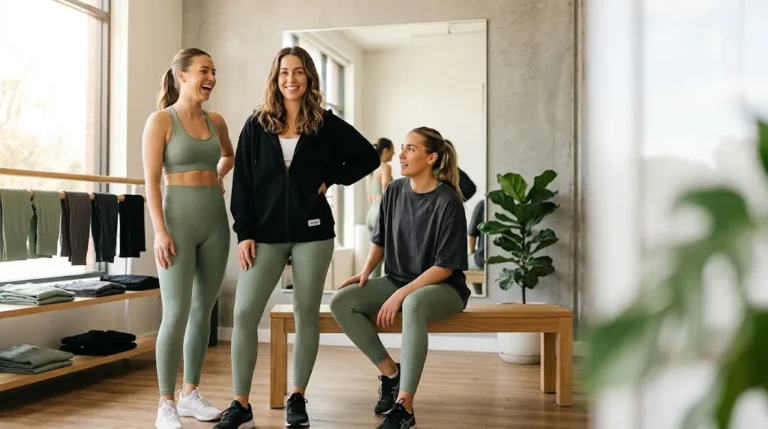
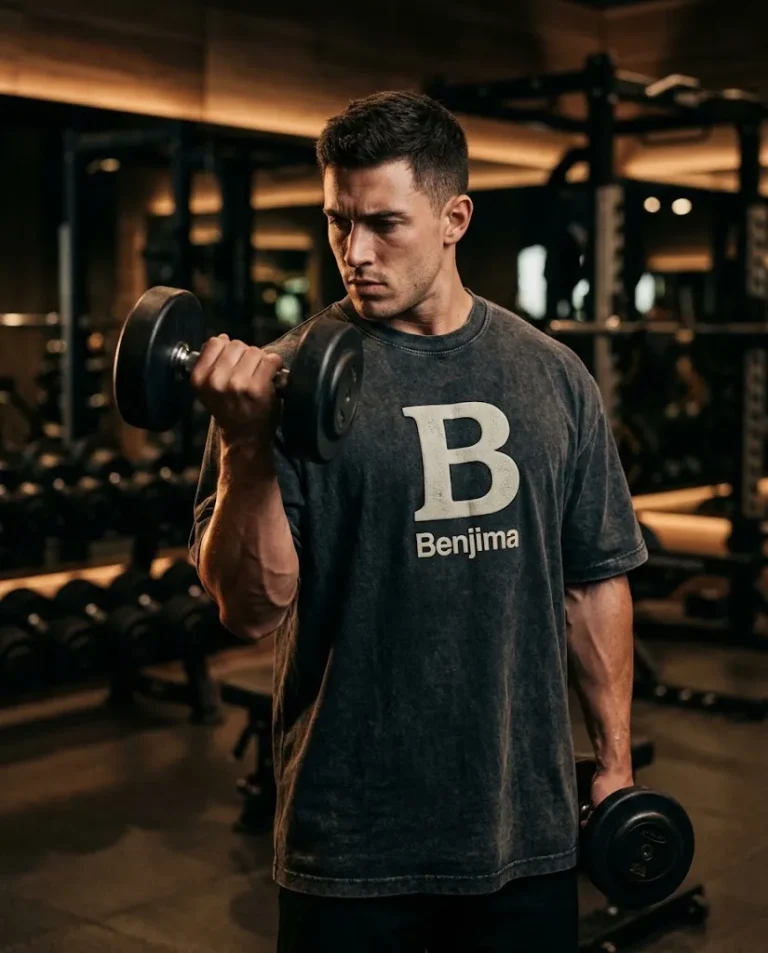
Select from versatile performance apparel categories engineered to launch, expand, and elevate your fitness brand catalog.
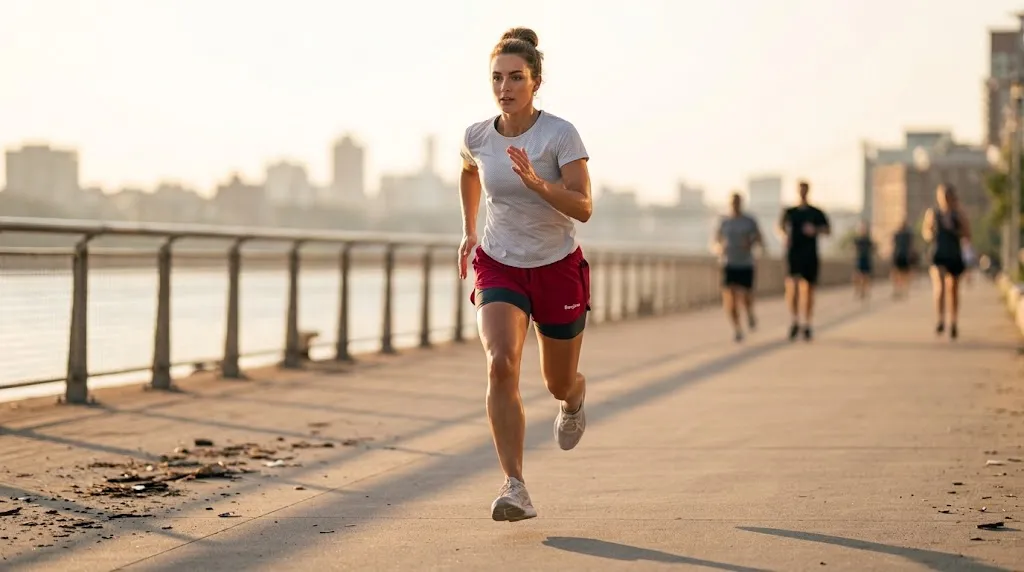
High-waisted squat-proof gym leggings, compressive sports bras, and ribbed biker shorts crafted on circular seamless knitting machinery.
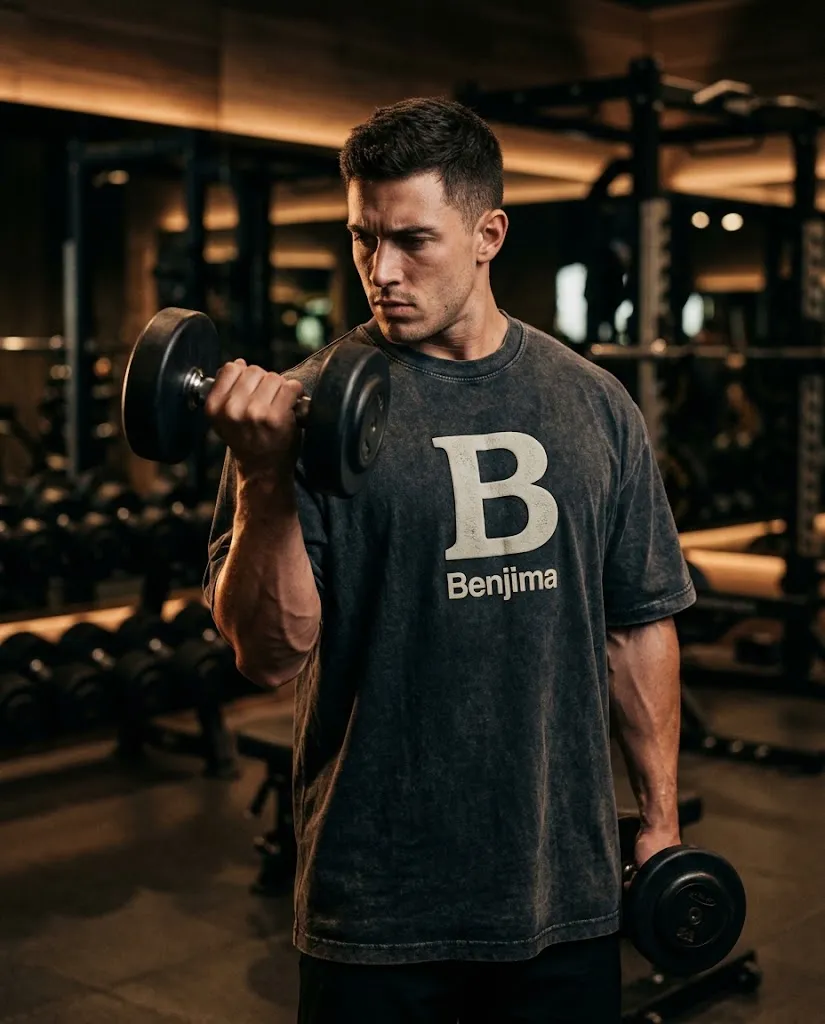
Contemporary drop-shoulder athletic t-shirts crafted from 240 to 300 GSM combed cotton featuring vintage acid washes or puff screen printing.
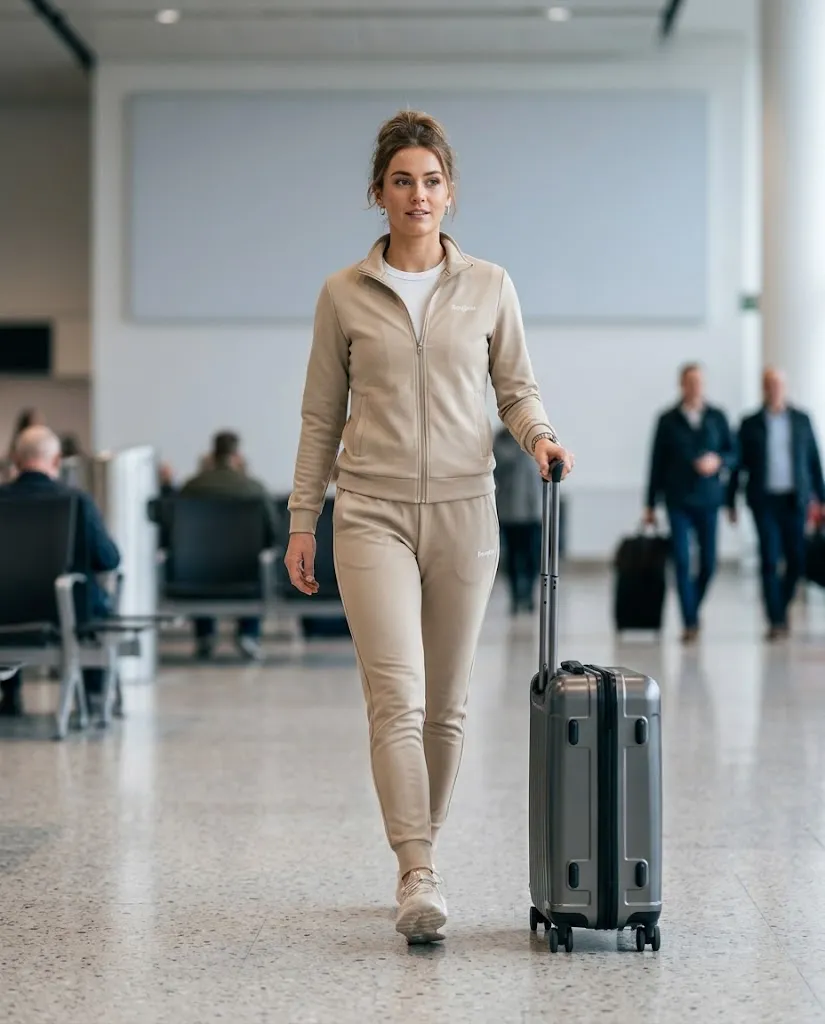
Heavyweight 360 to 450 GSM French terry and fleece pullovers with double-lined hoods, concealed zip pockets, and custom aglets.
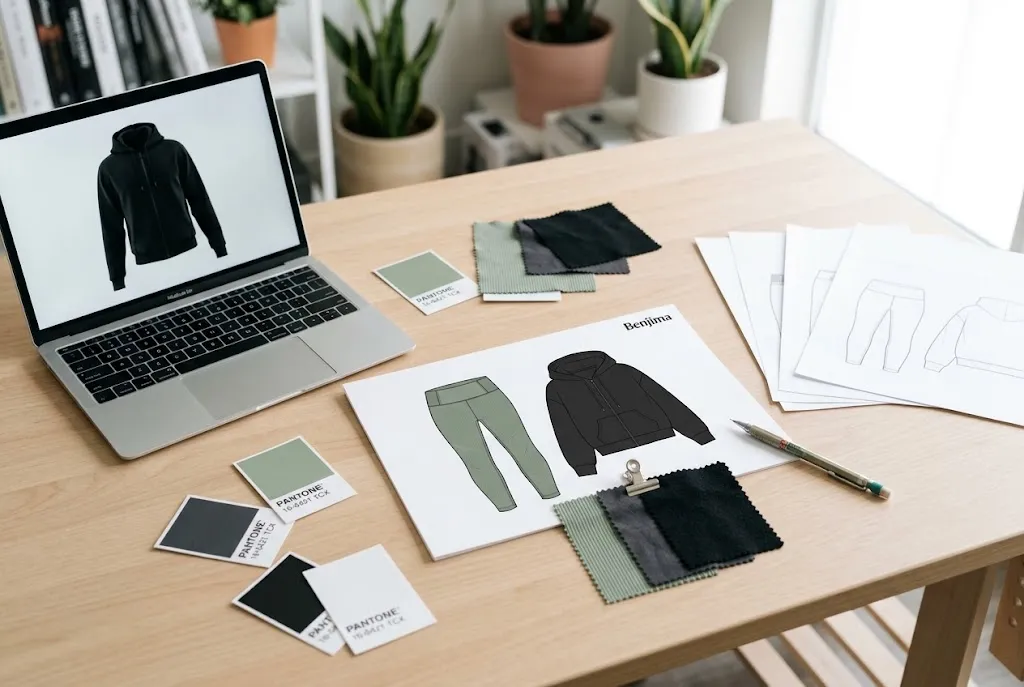
High-compression base layers engineered with flatlock stitching and muscle-supporting paneling for combat sports and running.
Tailored poly-tricot and stretch-woven travel sets designed for modern street-to-gym crossover aesthetic appeal.
Lightweight four-way stretch shorts with built-in compression liners, phone pockets, and customized towel loops.
Building an enduring activewear brand requires apparel that marries high-end fabric aesthetics with relentless physical durability. Our custom sportswear private label program utilizes specialized nylon-spandex, interlock polyester, and heavyweight combed cotton textiles engineered to retain elasticity and rich color depth. Reinforced six-thread flatlock seams and bar-tacked stress points eliminate blowouts along high-strain seams, ensuring your products exceed customer expectations.
We provide full pattern grading across youth, women, and men sizing charts, accommodating international size specifications (US, UK, EU, AU). Ergonomic shaping ensures flattering silhouettes, sculpted waistbands, and optimal athletic drape that flatter diverse body physiques. Each garment offers superior sweat management and breathability, allowing your brand's customers to train with total confidence.
Our factory handles every facet of the supply chain internally, from fabric sourcing and custom dying to branding hardware fabrication, cutting, sewing, and custom barcode packaging. This vertically integrated manufacturing model delivers meticulous quality oversight, guaranteed production schedules, and honest factory-direct pricing that powers brand profitability.
Brand founders and apparel buyers frequently ask how direct factory private label manufacturing delivers boutique-level finish and retail consistency across bulk production runs. By combining industrial CAD pattern drafting with premium custom branding hardware and rigorous multi-stage quality control, Benjima ensures your collections compete directly with established global activewear brands.
Off-the-shelf catalog blanks limit brand differentiation and restrict custom color palettes. We source bespoke fabric knits tailored to your exact GSM and hand-feel specifications, matching custom colors flawlessly using international Pantone (PMS) textile codes.
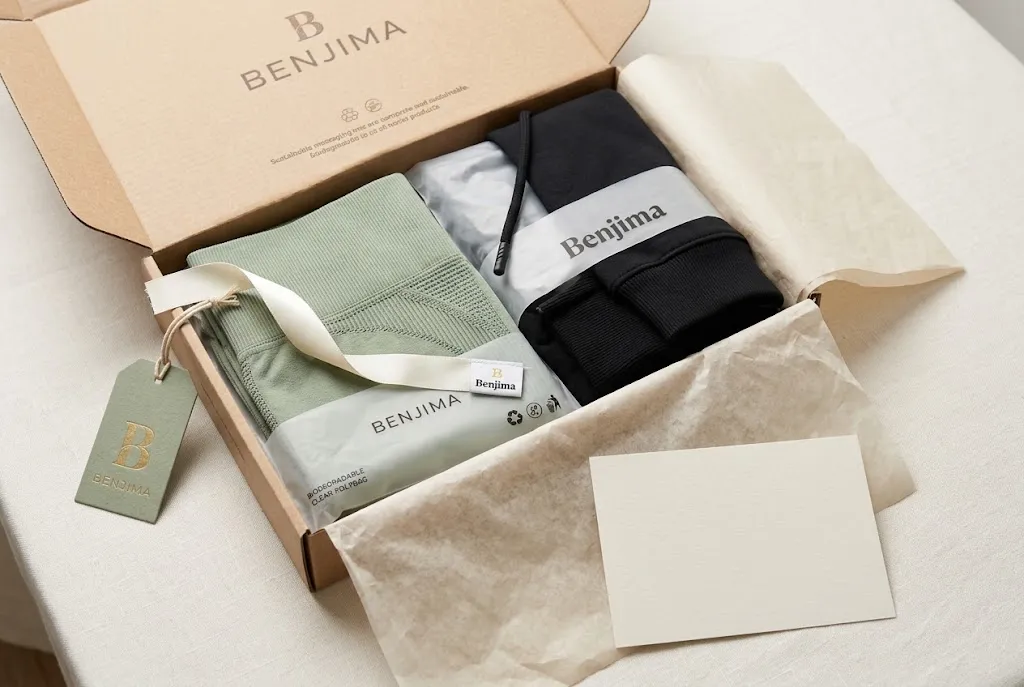
High-end branding details transform good athletic wear into luxury sportswear. We design and attach custom woven neck labels, heat-seal care tags, metal-tipped drawcords, rubber logo badges, and custom branded biodegradable polybags that deliver unforgettable unboxing experiences.
Our direct factory OEM engineering empowers activewear entrepreneurs to launch retail-grade sportswear lines that command premium pricing and lasting brand loyalty.
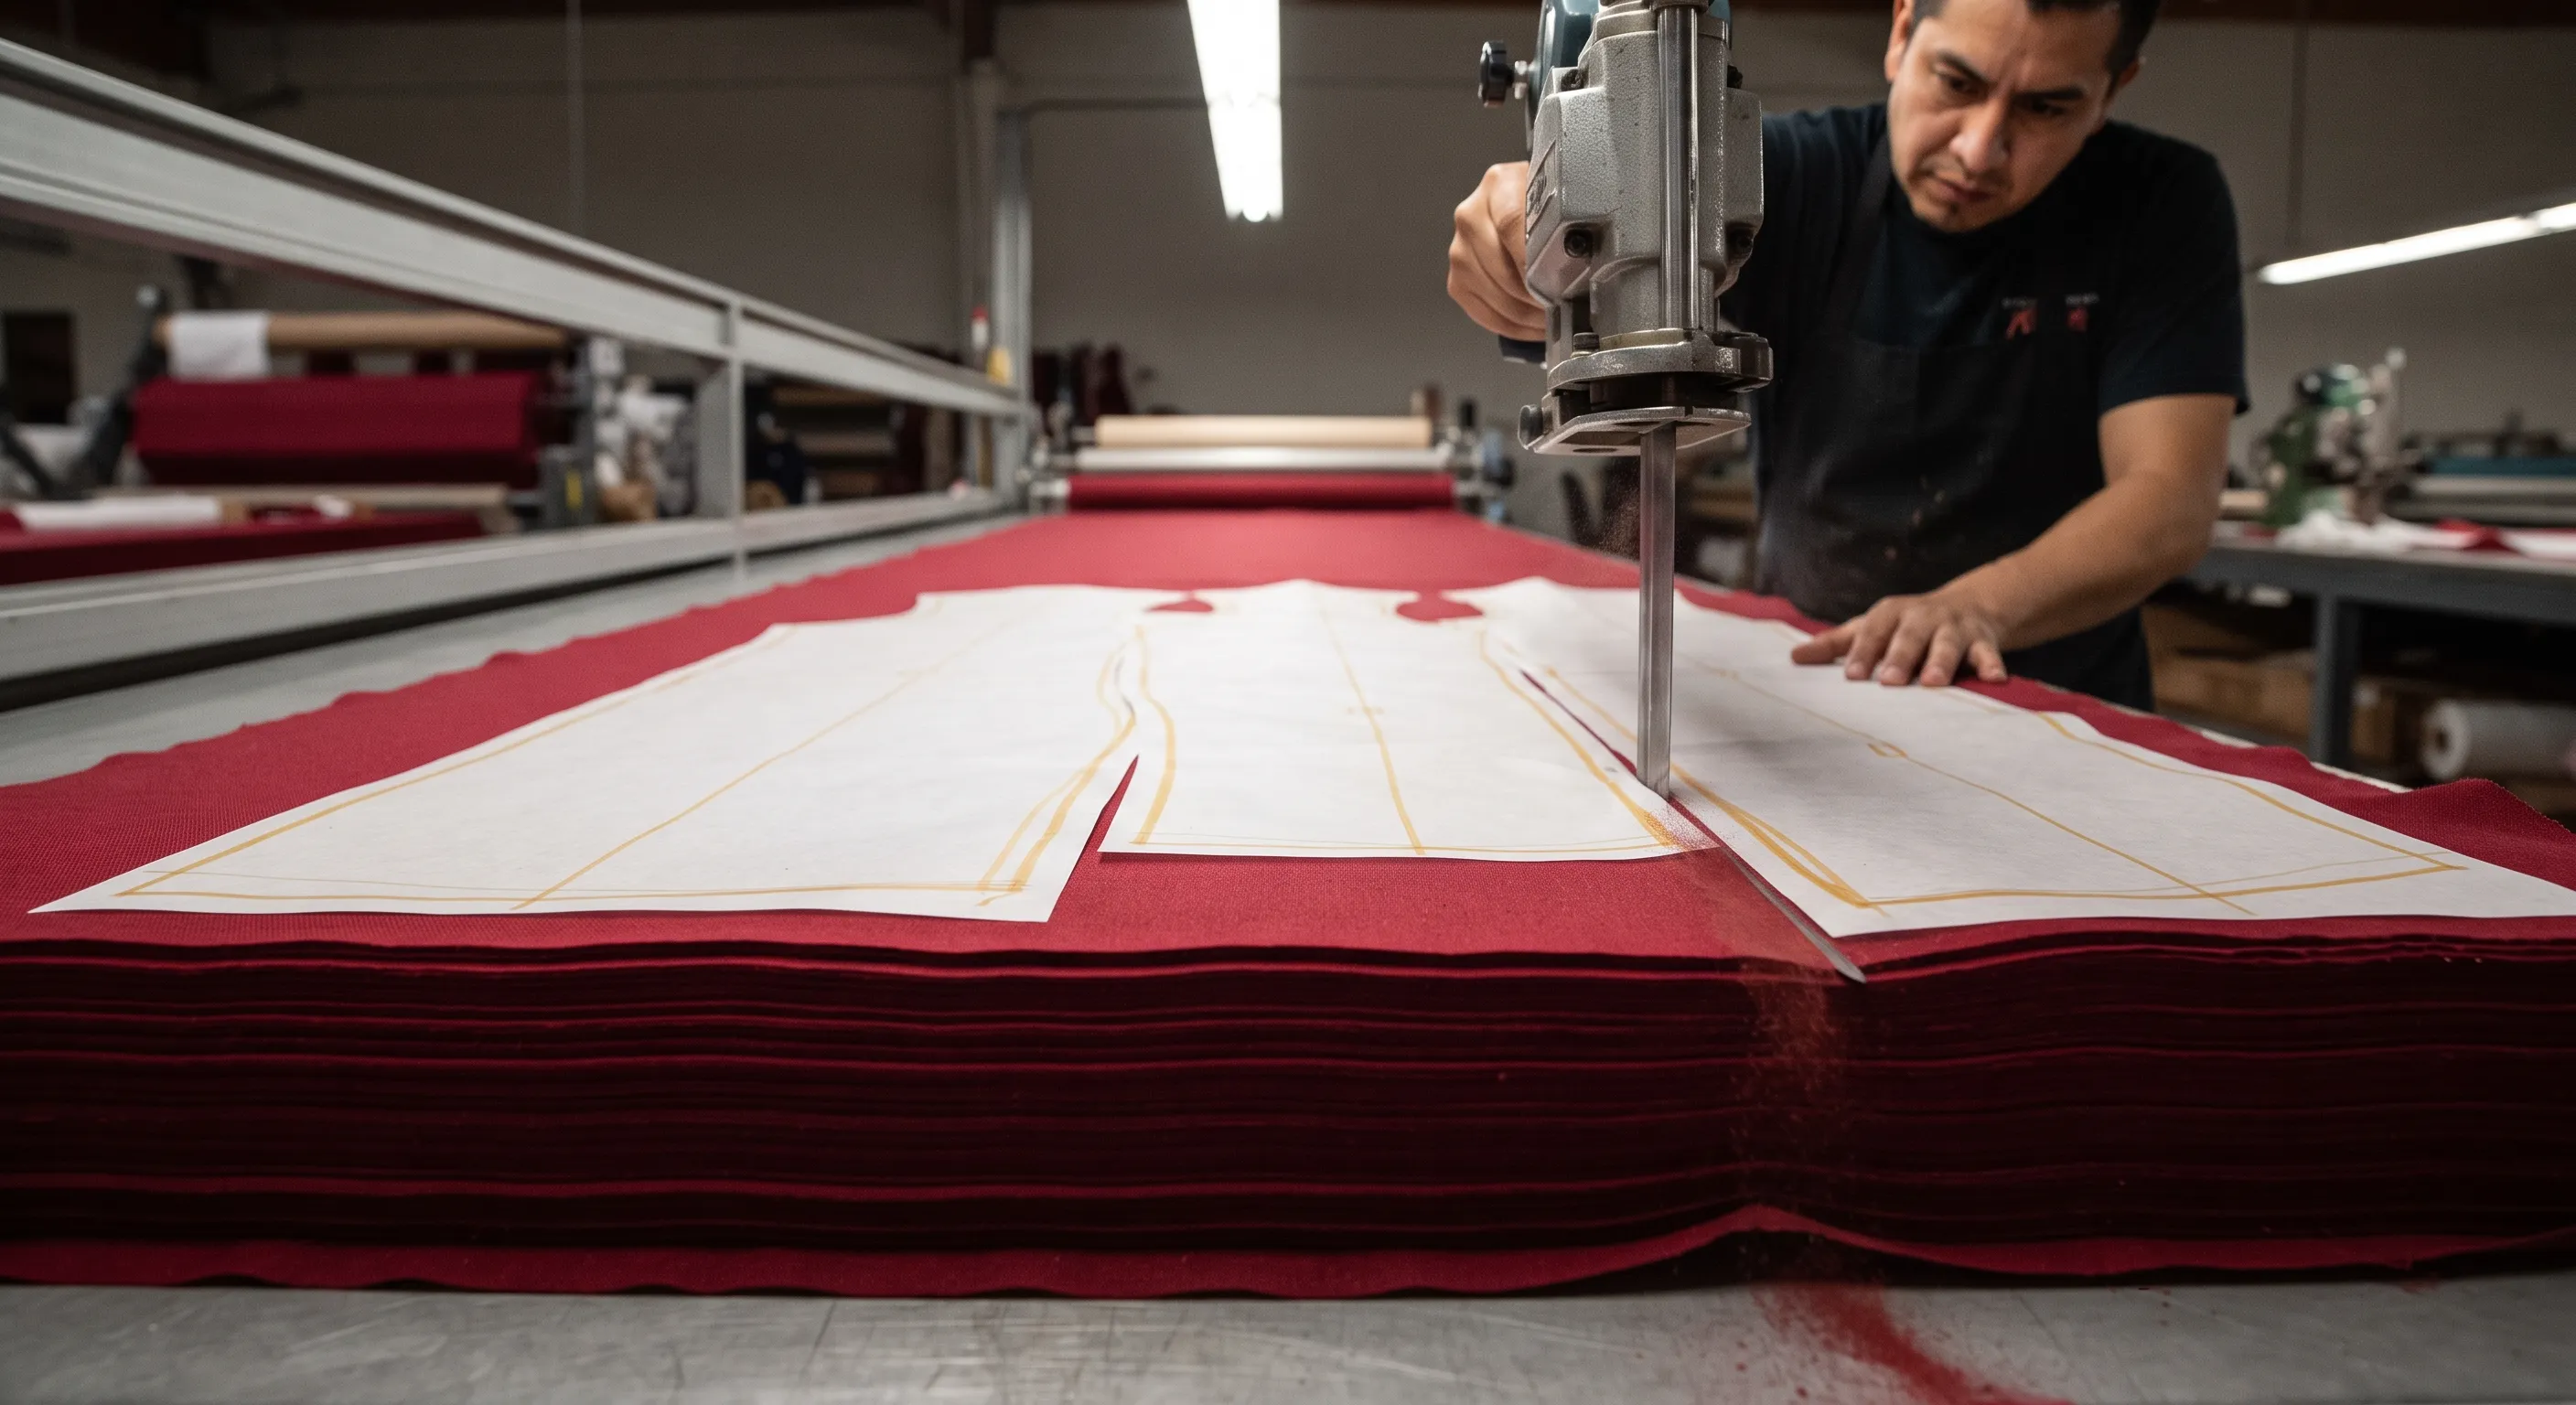
Inconsistent sizing across production runs destroys customer retention and inflates return rates. We use digital CAD marker drafting and precision laser cutting to guarantee identical fit across every unit, backed by inline inspection tables that check seam tolerances and stitching integrity.
Take a virtual tour through our modern apparel factory to see how custom private label sportswear is designed, cut, sewn, and branded for emerging athletic labels.
Engineered from the ground up to deliver retail-grade construction, bespoke brand identity trims, and high profit margins for your athletic label.
Full pattern development, bespoke tech packs, and custom fabric knitting built to your brand's exact design specifications.
Custom woven neck labels, heat-seal care tags, branded aglets, custom hang tags, and branded polybag packaging.
Expertise in 3D high-density embroidery, full dye sublimation, puff screen print, silicone gel printing, and tackle twill.
Multi-stage factory inspection protocols checking seam strength, fabric flawlessness, and dimensional sizing accuracy.
We partner with activewear entrepreneurs and businesses worldwide, delivering custom branded apparel suited for retail brands, fitness clubs, and creator merchandise.
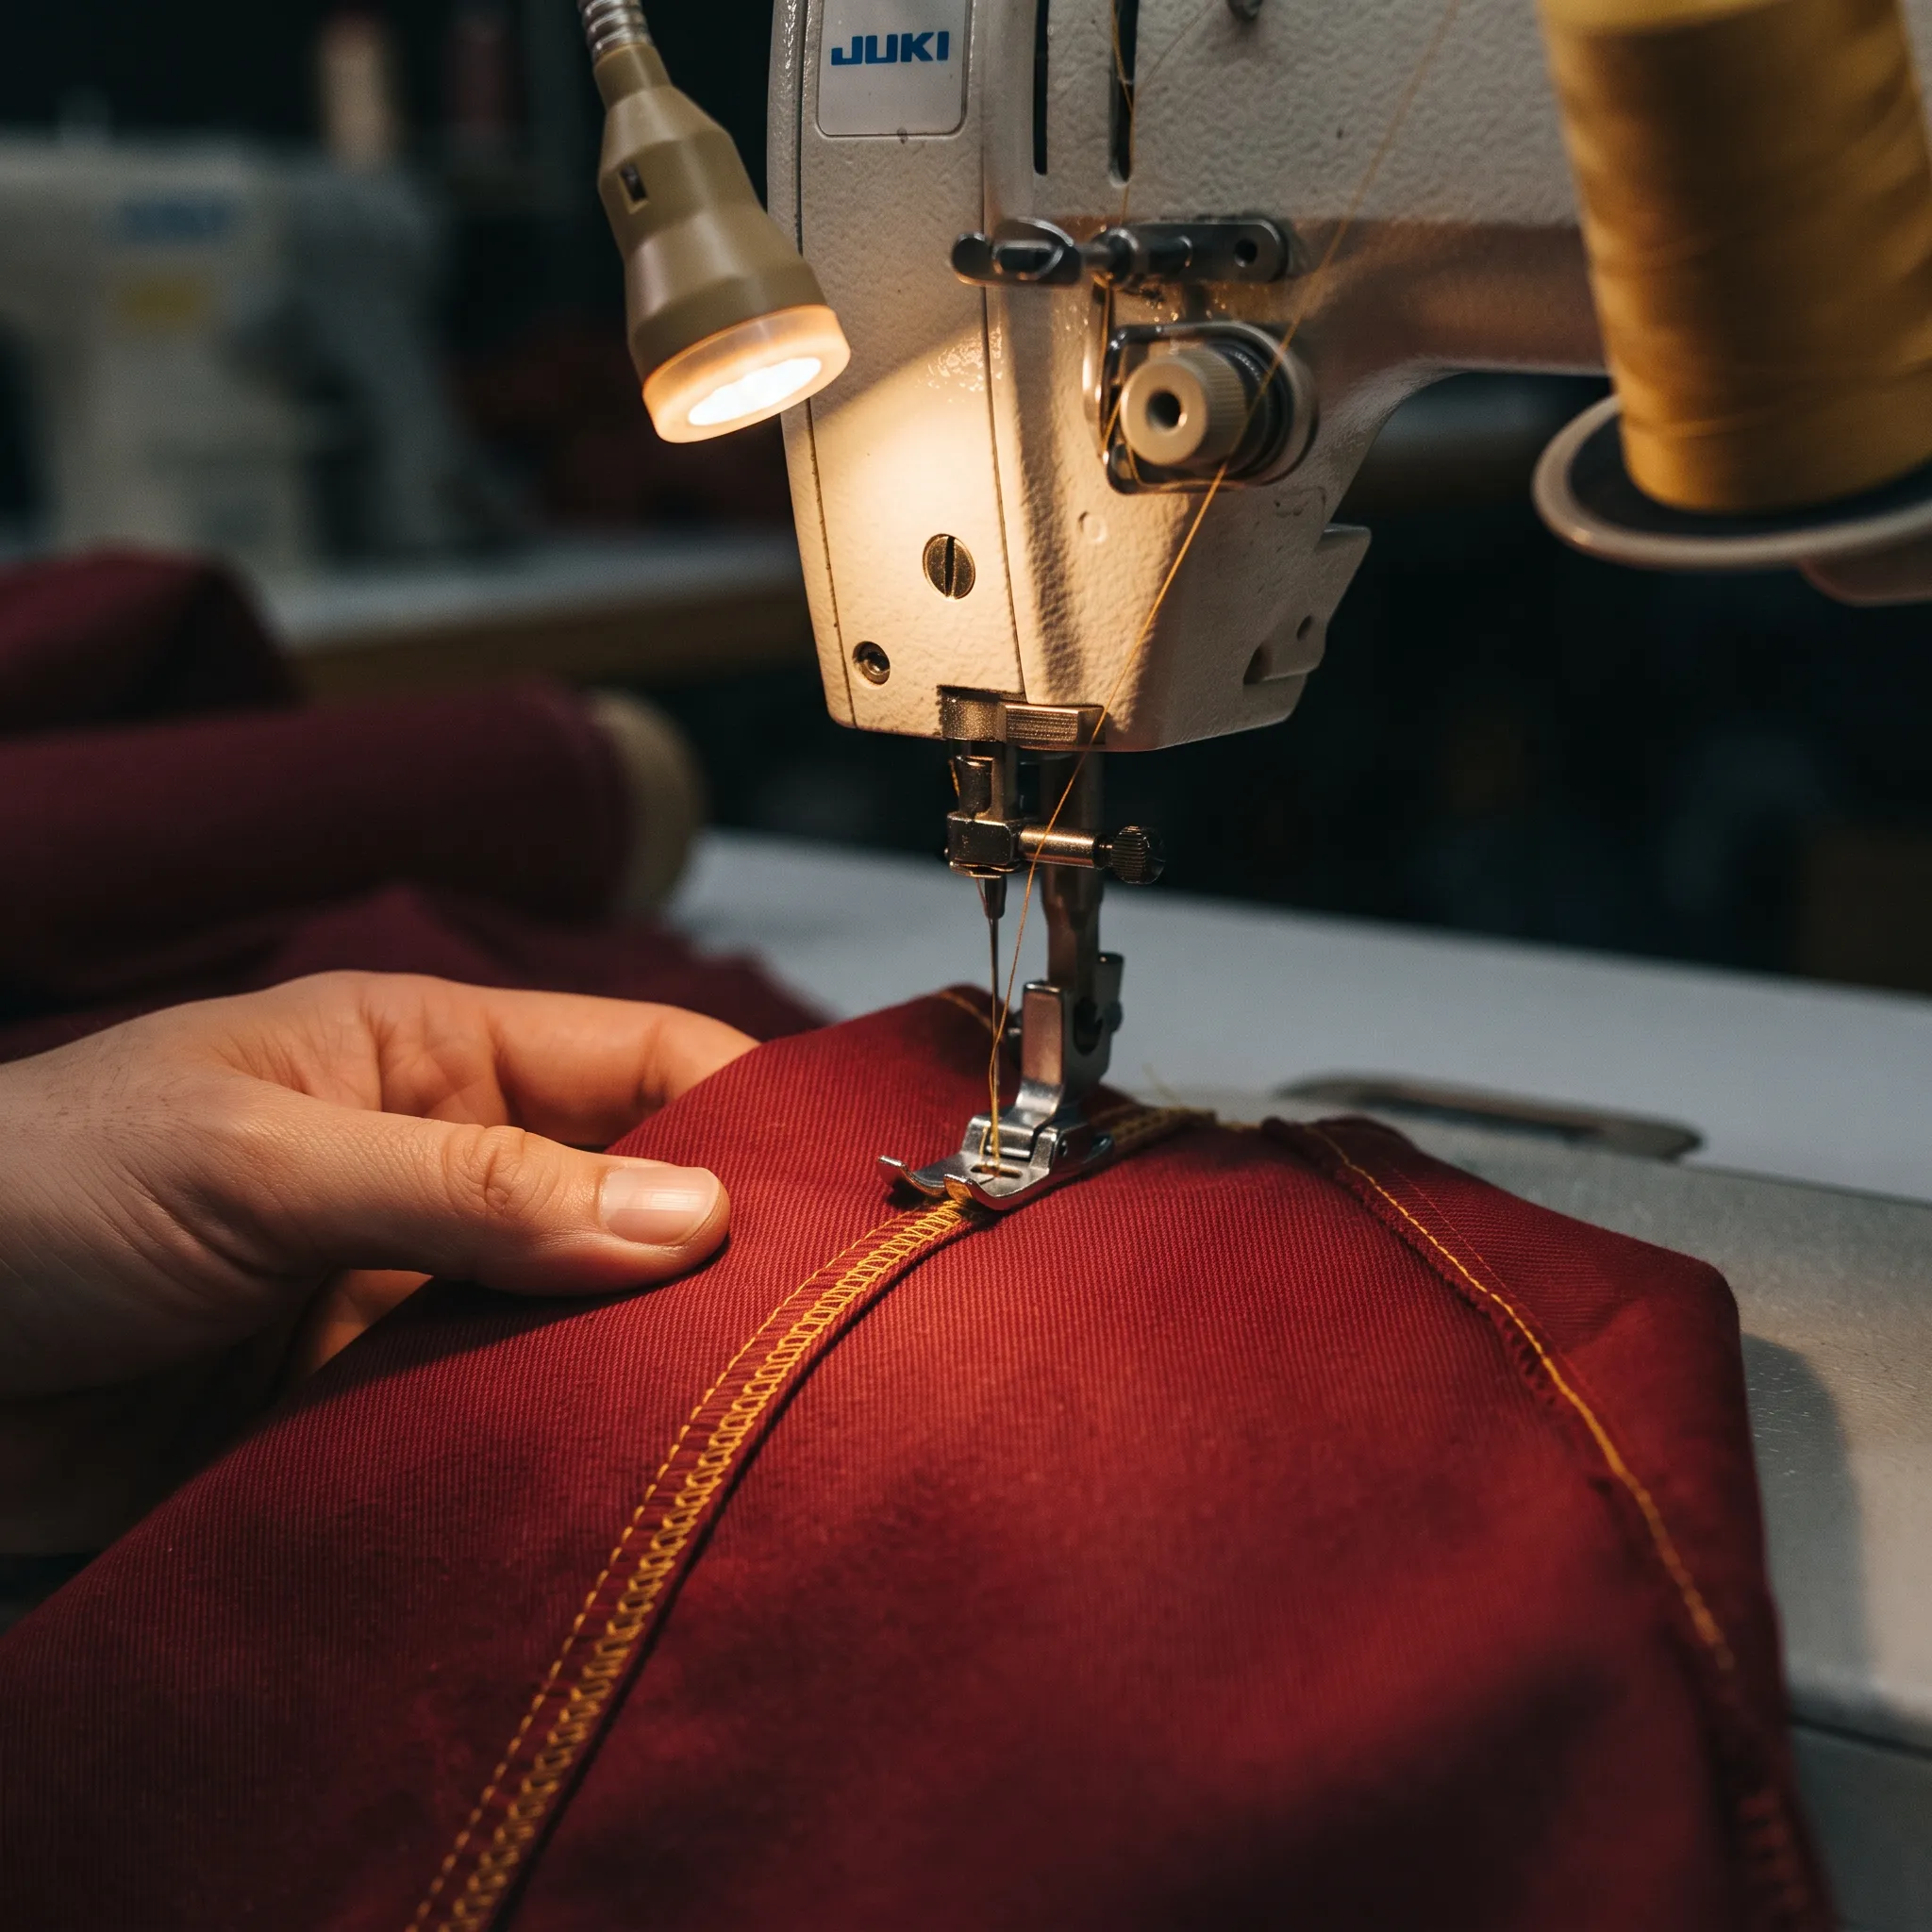
Follow our simple five-step manufacturing workflow designed to take your athletic apparel brand from creative sketch to retail shelf.
Start your orderShare your proprietary sketches, tech packs, measurement charts, and packaging design requirements.
We manufacture physical pre-production prototype samples and woven label mockups for physical review.
Validate fabric hand-feel, stretch recovery, and stitch aesthetics before authorizing bulk production runs.
Our lines cut, sew, print, and finish your custom garments under strict AQL 2.5 quality control standards.
Garments receive custom neck tags, branded hangtags, and barcoded polybags shipped to your fulfillment hub.
We offer woven labels, heat-transfer tags, branded hangtags, embossed aglets, silicone chest patches, and custom biodegradable polybags.
Yes, we offer comprehensive full-package private labeling solutions including woven neck labels, heat-transfer satin tags, custom branded cardboard hang tags, barcode stickers, and custom printed biodegradable zip polybags.
Yes, we create complete pre-production physical prototypes and fit samples so brand founders can evaluate fabric hand-feel, fit ergonomics, stitching quality, and embellishments before committing to bulk manufacturing runs.
Standard sample creation takes seven to ten business days. Full bulk production takes two to three weeks from final sample approval and sizing confirmation, with express shipping options available worldwide.
Yes, our dye house matches exact Pantone (PMS) textile color codes for fabric dyeing, custom zipper tapes, rib knit trims, and screen printing inks, ensuring complete brand color consistency across product lines.
Yes, our in-house apparel design team can convert rough sketches, reference photos, or sample garments into professional CAD tech packs with complete size grading charts for factory production.
| Turnkey Production Capabilities | Full OEM/ODM cut-and-sew, tech pack drafting, sample prototyping |
|---|---|
| Custom Label Packaging | Woven neck tags, heat seals, custom hang tags, biodegradable polybags |
| Custom Grading Chart | Complete size grading from XXS to 5XL tailored to brand demographics |
| Brand Production Lead | 7-10 days for sample prototypes; 14-21 days for bulk production |
| Private Label MOQ Terms | 20-50 units for custom cut-and-sew; zero MOQ for sublimated capsules |
Submit your custom tech packs for bespoke label development, prototype review, and scalable production terms.
Tell us the garment, the quantity and the date. That is enough for a costing.
We reply within one working day. No mailing list.
A written quote will reach you within one working day.